

Troubleshooting for reaming
Main problems
- Spindle or tool run-out is too high
- Wrong cutting data
- Built-up edge
When solving a problem:
- Look at the whole system (tool, clamping, spindle, coolant etc.)
- Always change only one parameter at once
Oversized bore
| 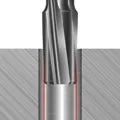 |
Undersized bore
| 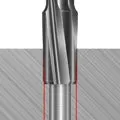 |
Tapered bore
| 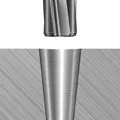 |
Bad surface finish bore
| 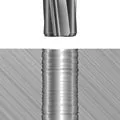 |
Wrong position of the bore
| 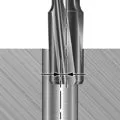 |
Bore is convex or oval
| 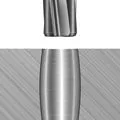 |
Chattermarks in the bore
| 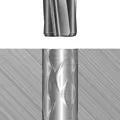 |
Tool clamps and breakage
| 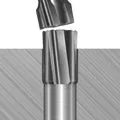 |
Feed grooves in bore
|  |
Chip removal problems
| |
Related information
Step and chamfer drilling
Step drilling and chamfer drilling Chamfer drilling Step drilling or step and chamfer... chevron_right
Drilling
Drilling a hole Drilling is often carried out late in the manufacturing process... chevron_right
Radial adjusted drilling
Radial adjusted drilling Radial adjusted drilling is only possible using indexable... chevron_right
CoroDrill® DE10
Exchangeable-tip drill for high-volume hole making Tired of the usual trade-offs?... chevron_right
