 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right

CoroMill® MS40
The ultimate tangential milling solution
HRSA HPC split casing
Productivity

| Component: | HPC casing |
| Material: | S2.0.C.NS, Inconel 718 |
| Operation: | Face milling |
| Machine: | Vertical 3-axis machining centre, BT50 |
Challenge: For meeting a production ramp-up, higher productivity with machining security is required.
Result: With CoroMill® MS40, productivity was improved by +90% and cycle time was reduced by 42% per component.
| Competitor | Sandvik Coromant | |
| Tool | - | MS40-R050Q22-13H |
| Insert | - | MS40-130608E L40 1040 |
| DCX, mm (inch) / Zn | 63 (2.48) / Z4 | 50 (1.97) / Z6 |
| vc, m/min (ft/min) / n rpm | 20 (66) / 101 | 20 (66) / 127 |
| fz, mm/z (in/z) | 0.1 (0.0039) | 0.1 (0.0039) |
| vf, mm/min (in/min) | 40 (1.575) | 76 (2.005) |
| ap / ae, mm (inch) | 0.9 / 40 (0.035/1.18) 250 (9.84) x2 flanges | 0.9 / 40 (0.035/1.18) 250 (9.84) x2 flanges |
| Coolant | Emulsion (external) | Emulsion (external+internal) |
| MRR cm3/min (in3/min) | 1.46 (0.088) | 2.75 (0.168) |
| Cycle time, min | 13 | 7.6 |
| No of components | 1 | 1 |
General engineering
Tool life increase
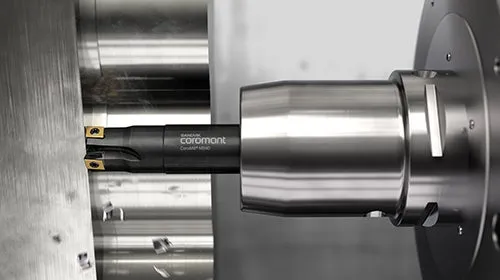
| Component: | Tool block blank |
| Material: | P2.2.Z.AN (50CrV4), 220HB |
| Operation: | Rough shoulder and face milling |
| Machine: | BFW VMC, BT40 |
Challenge: Improve tool life and control insert wear pattern with minimum force on the spindle in 4th axis UCAM.
Result: Minimal insert wear pattern after 90 components in dry cutting condition. The customer is very satisfied with CoroMill® MS40 insert wear pattern and edge security.
| Competitor | Sandvik Coromant | |
| Tool | - | MS40-R050Q22-13H |
| Insert | - | MS40-130608M-M50 1230 |
| DCX, mm (inch) / Zn | 50 (1.97) / Z4 | 50 (1.97) / Z6 |
| vc, m/min (ft/min) / n rpm | 164 (538) / 1050 | 164 (538) / 1050 |
| fz, mm/z (in/z) | 0.12–0.14 (0.0047–0.0055) | 0.08–0.095 (0.0031–0.0037) |
| vf, mm/min (inch/min) | 500–600 (19.7–23.6) | 500–600 (19.7–23.6) |
| ap / ae, mm (inch) | 0.5 / 19–24 (0.0200 / 0.75–0.945) | 0.5 / 19–24 (0.0200 / 0.75–0.945) |
| Coolant | Wet, external | Dry |
| Insert tool life, min | 120 | 270 |
| No of components | 40 | 90 |
CGI cylinder head
Tool life increase
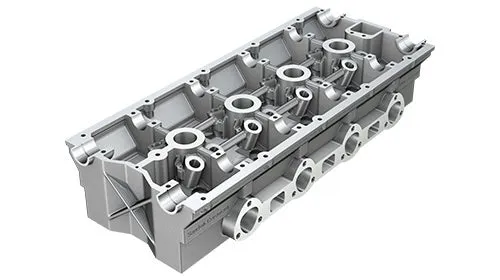
| Component: | Cylinder head for six cylinders |
| Material: | K4.2.C.UT (EN-GJV-440) |
| Operation: | Face milling |
| Machine: | Horizontal MC, HSK-100A |
Challenge: The customer is unsatisfied with the current tangential cutter and its poor tool life in rough face milling operation of cast skin in CGI.
Result: With CoroMill® MS40 tool life increased by 40% and was achieved without issues.
| Competitor | Sandvik Coromant | |
| Tool | - | MS40-R050Q22-13H |
| Insert | - | MS40-130608M-M50 GC4330 |
| DCX mm (inch) / Zn | 50 (1.97) / Z6 | 50 (1.97) / Z6 |
| vc, m/min (ft/min) | 180 (590) | 180 (590) |
| fz, mm/z (in/z) | 0.16 (0.006) | 0.16 (0.006) |
| ap, mm (inch) | 2 (0.078) x3 passes | 2 (0.078) x3 passes |
| Coolant | Wet | Wet |
| Insert tool life, min | 173 | 242 |
| No of components | 10 | 14 |
Aerospace martensitic 410
Tool life increase
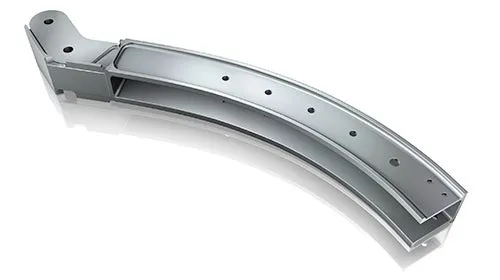
| Component: | Aerospace component |
| Material: | P5.0.Z.AN, S.S. 410 in annealed condition, 220HB |
| Operation: | Mill rough out 90° shoulder |
| Machine: | Doosan MV4020 |
Challenge: To replace the use of a solid carbide end mill. Several 90° solutions from other competitors have been tested without success.
Result: 68 parts completed and 1081 cm3 (66 in3) of material removed, no change in insert edge, machine sound or chip color. The customer would have used at least two end mills (approximately $50.00 per piece) to complete the same work.
| Existing solution | Sandvik Coromant | |
| Tool | - | MS40-R025A25-09H |
| Insert | Solid round mill | MS40-090404M-M40 1230 |
| DCX mm (inch) / Zn | 12.7 (0.500) / Z4 | 25 (0.9843) / Z4 |
| vc, m/min (ft/min) | 141 (464) | 260 (853) |
| fz, mm/z (in/z) | 0.1 (0.0039) | 0.18 (0.007) |
| ap / ae, mm (inch) | 10.6/1.9 (0.400/0.075) | 5.08/1.9 (0.200/0.075) |
| Coolant | Wet | Dry |
| Insert tool life, min | 102 | 204 |
| No of components | 34 | 68+ |
