

Think small
A long slowdown in the oil industry prompted Knust-Godwin LLC to try another direction. Sandvik Coromant was there to help.
Knust-Godwin, a division of Schoeller Bleckmann Oilfield Equipment AG, is a precision machining company located in Katy, a small town 30 miles west of Houston, Texas. It specializes in large, complex parts for oilfield instrumentation. But with the recent downturn in the oil industry, Knust-Godwin management agreed the company should work to diversify its customer base. This would keep the doors open during lean times and keep the business primed for when the industry bounced back.
Besides the oil industry, Knust-Godwin services the semiconductor, medical, seismic and geophysical industries. Its capabilities range from 5-axis CNC machining and milling/turning to gun drilling, laser and electron beam welding, EDM (electrical discharge machining) and even additive manufacturing. Many of the machine tools in its 22,000-square-metre facility are larger than a tractor-trailer and are able to drill holes up to 9.5 metres deep, turn shafts nearly 6.4 metres long, and mill parts 11 metres across. An average workpiece measures five feet 1.5 metres long and six inches 15 cm in diameter (although some are far larger), is made of Inconel, Hastelloy or a similar tough material, and might require 50 to 60 hours of machining; several hundred hours of machine time per part is not uncommon.
Yet when the opportunity to machine wristwatch parts came along some smaller than 10 mm in diameter – Knust-Godwin management said “Why not?”
There’s a precedent. Knust-Godwin is the result of a merger between two longstanding Houston-area machine shops, Knust and Godwin. Godwin focused on general machining, but Knust began as a precision watchmaker. Both came to be experts in oil and gas machining and were eventually acquired by Schoeller Bleckmann Oilfield, which merged the two into a single company during the recent oil and gas slump.
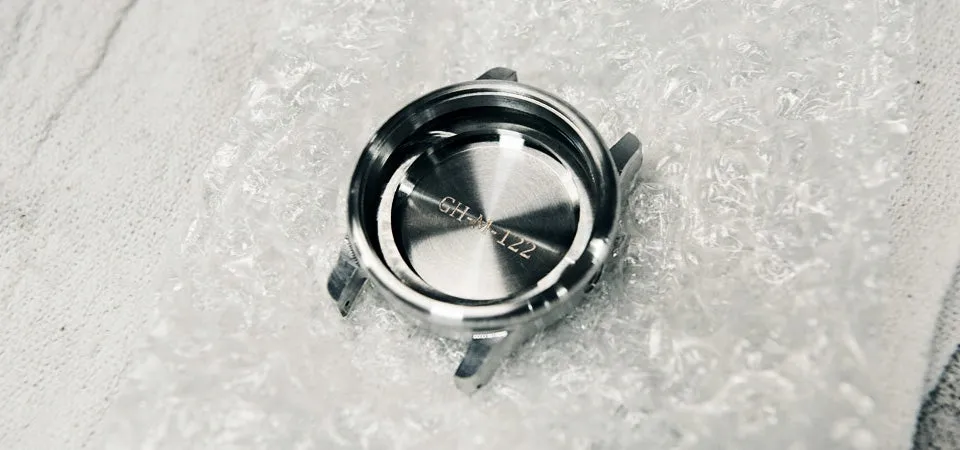
Meanwhile, programmer Cameron Birse learned of a startup in Portland, Oregon, offering a new line of high-end timepieces – VERO Watches – that was struggling with fit and finish problems on prototypes from a local machine shop. It was looking for an alternate source. Birse alerted Sales Manager David Prickett of the opportunity, the quote package was delivered, and Knust-Godwin found itself back in the watchmaking business.
“Many of us were unaware of our roots,” says programmer Chris Hurst. “Then one of the old-timers from Knust saw the drawings. ‘We used to make parts like that,’ he said. It turns out we’d come full circle.”
Needless to say, machining technology has changed substantially in the past 50 years. Knust-Godwin quickly learned that what works for large parts is less effective on very small ones. Even though Hurst and his team were quite familiar with the difficulties of titanium and high-nickel alloy machining, the far more machinable 316 stainless steel, of which the watch bodies were made, was destroying tools quickly enough that acceptance of future orders was in question.
“We started with an order for two sets of prototype parts,” says Hurst. “This includes the watch case itself, plus the back piece, the bezel, the crown and a few other pieces. The biggest was around 32 mm across, while the smallest was a washer just 4.5 mm in diameter.”
Most of the parts were machined on one of Knust-Godwin’s DMU 125 monoBLOCK universal machining centres from machine builder DMG MORI. With a work volume of 870 cubic centimetres and a table load capacity of more than 6,000 kilograms, the DMU was obviously overkill for the small parts, but the machine’s superb accuracy and 10,000 r/min spindle made it the logical choice for the project.
Despite the high level of machining technology, Hurst says, they soon found themselves in trouble. “I don't mind challenges,” he says. “We’re used to high-stakes machining. But our tool life on the prototypes run was so poor, we knew the production order would be miserable. Most of the tools couldn’t complete a single part without needing to replace it. We had to do something different.”
VERO Watches enthusiastically accepted the prototypes, and Knust-Godwin was soon facing an order for 105 complete watch sets. They called Grant Gregory, account productivity engineer for Sandvik Coromant.
Gregory recommended several changes. The ER-style collet holders used to hold the various endmills and drills were replaced with CoroChuck® 930 high-precision hydraulic chucks, greatly improving tool runout and security. Instead of a 12.7-mm diameter solid carbide endmill, roughing was done with a CoroMill® 390-07 indexable cutter with GC1130 grade carbide inserts. And the 1.6-mm ballnose “import” endmills were replaced with CoroMill Plura 1630 grade cutters.
The results were dramatic. Hurst says he was previously using two ballnose endmills – a regular length and a stub – to semi-finish and finish machine each watch body. By switching to a Plura ballnose endmill held in a hydraulic CoroChuck, tool life increased to 80 parts per endmill. “It was an unbelievable improvement,” he says. “Feeds and speeds, depth of cut – everything was the same, except the one Plura endmill was actually doing 90 percent of the finishing work on the outside of the part. It came out to an 8,000 percent productivity increase per tool.”
The CoroMill indexable cutter produced similar results, roughing out the entire 105-piece order on a single set of inserts. Tool life improved even with the legacy tooling. In one case – a 0.813-mm square nose endmill responsible for cutting a groove on the crown interior – tool life improved by 400 percent by switching to the CoroChuck. “That was the smallest improvement we saw with any of the tools,” Hurst says. “We’d long suspected that better tooling would make a difference, but never had this sort of head-to-head comparison.”
Granted, the Sandvik endmills cost substantially more than the legacy tooling, but the cost per part still came in at roughly 1/16th that of the less-expensive cutters, Hurst says, not even counting the disruption and downtime of frequent tool changes due to dull cutters.
Birse agrees. “Tool life was definitely an issue,” he says. “We had all these three-dimensional surfaces blending into other three-dimensional surfaces, so any time you had to change tools it was a big deal. I think much of the improvement came from the carbide, but those hydraulic pencil-style holders definitely helped as well. It was a massive benefit.”
Knust-Godwin delivered the watch parts as promised. And because of the greater tool life and surface finish achieved with the Sandvik Coromant tooling, Hurst and others there are looking forward to the next order. “The Houston machining industry has never been very good about diversification,” he says. “It’s always been about the oilfield, so when things slow down it’s tough to transition into different markets and actually make it successful. We’ve learned some things from this job and that’s always a good thing. And even if we never make another watch body again, we’re going to be re-evaluating our cutting tools and how we're holding them.”
Footnote: This article first appeared in a slightly longer version in Manufacturing Engineering magazine
